
A low-PIM value on a datasheet is useful, but it is not enough to qualify a passive component. The result only has meaning when it is tied to a defined product, frequency range, connector configuration, test-tone power, measurement method, and acceptance limit.
At RFCOM, we approach low-PIM passive-component quality as a controlled delivery chain. It starts with the project requirement, continues through product-family-specific design and assembly controls, and ends with an agreed inspection and acceptance plan. This matters because a component that looks suitable by headline specification can still be a poor fit if its test conditions or mechanical configuration do not match the actual RF path.
The practical goal is not to promise “zero PIM.” It is to reduce avoidable uncertainty and give the buyer enough information to select, review, and accept the right component for the application.
1. Start with the requirement, not the headline number
Low PIM is not a standalone purchasing category. A power splitter, directional coupler, tapper, hybrid combiner, load, or attenuator performs a different function in the network, and each must be evaluated against the RF design.
Before recommending a model, RFCOM reviews the information that defines the application:
- component type and port configuration;
- operating frequency range;
- connector type and gender;
- average and peak power requirements;
- target PIM level and the required test conditions;
- coupling, attenuation, split, isolation, insertion-loss, or return-loss requirements, as applicable;
- indoor or outdoor environment;
- sealing, temperature, corrosion, mounting, and mechanical constraints, where relevant; and
- quantity, labeling, packing, documentation, and acceptance requirements.
This first step prevents a common problem: comparing two PIM figures that were obtained under different conditions. The current IEC 62037-1:2025 standard, for example, treats test frequency, power, setup, and reporting parameters as part of a properly defined PIM measurement. It also makes an important distinction: PIM measurement does not, by itself, establish long-term product reliability.
For that reason, RFCOM confirms the applicable model and test basis before a product-level PIM claim is used in a proposal, drawing, or tender response.
2. Use design choices that reduce unnecessary variability
Passive intermodulation can be influenced by mechanical contacts, joints, conductive surfaces, and connector interfaces. The design objective is therefore not simply to meet an electrical value once. It is to make the construction repeatable for the selected product family.
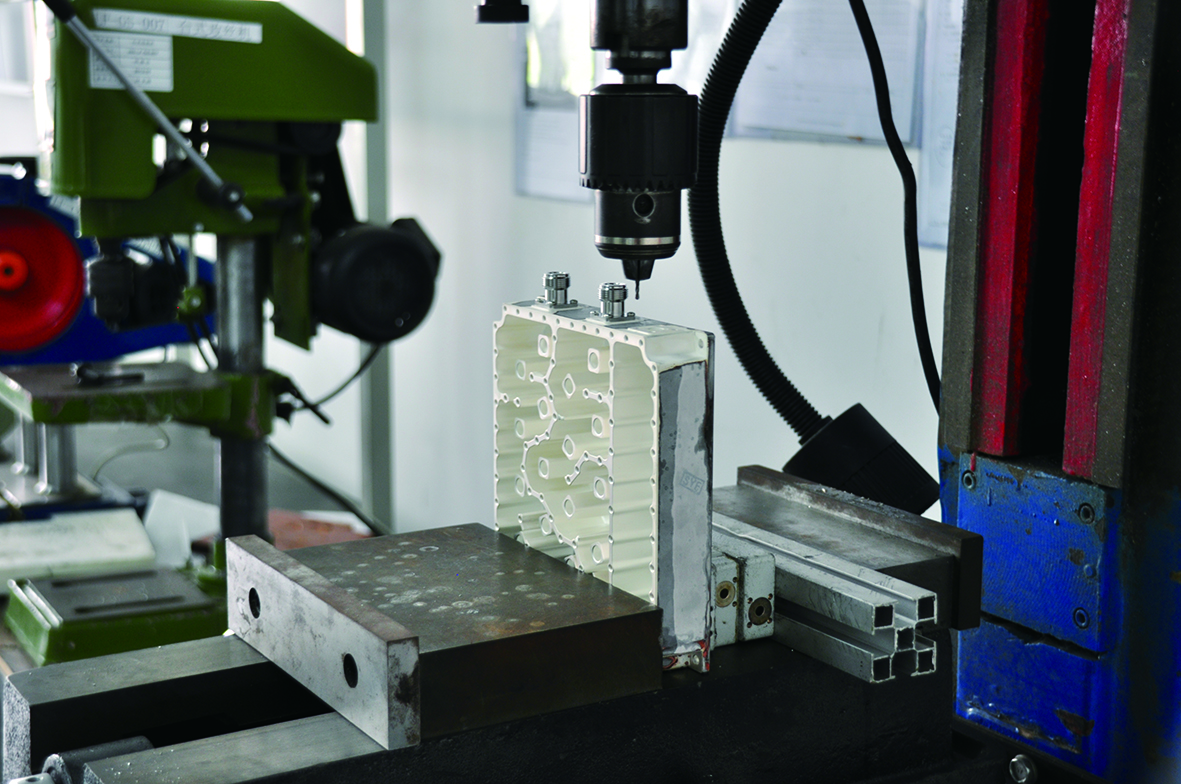
Where the product design allows, selected RFCOM passive components use an integrated cavity structure with fewer internal solder joints. Selected designs also use silver-plated internal surfaces and connector interfaces chosen for the required RF and mechanical configuration. These choices can reduce avoidable sources of variation, but they are not universal across every RFCOM product.
The exact construction must always be checked against the approved model specification. A design detail that is suitable for one splitter or coupler family should not be copied into a claim for another family without evidence.
3. Keep assembly controls tied to the product family
Good design can be undermined by inconsistent assembly. Contact condition, alignment, joint quality, and the way interfaces are handled can all affect the finished RF component.
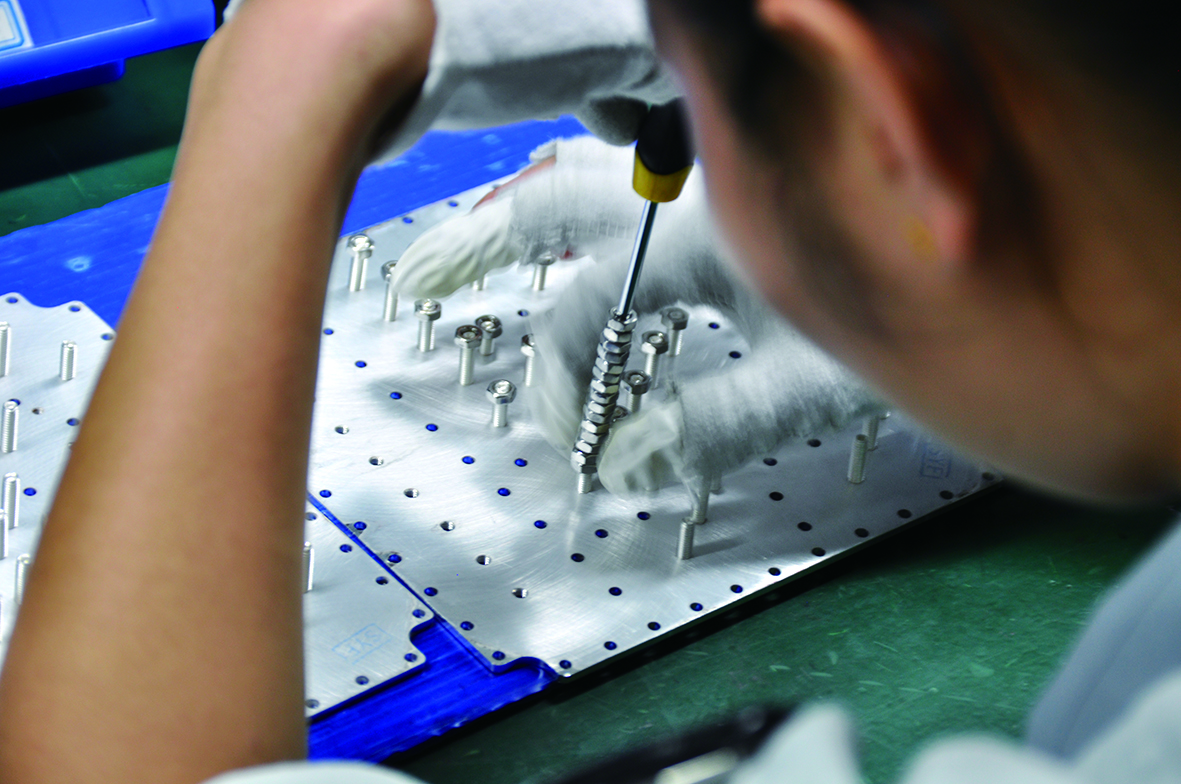
RFCOM uses controlled assembly for applicable passive-product families. The relevant work instructions and inspection points depend on the construction of the selected model. That product-family boundary is important: we do not describe one assembly sequence as if it applies to every splitter, coupler, tapper, combiner, load, and attenuator.
For a qualification project, buyers should ask which process controls apply to the proposed model and which characteristics are verified during production. If a tender requires a specific inspection record, traceability field, or witness point, it should be agreed before the order is released—not added after production.
4. Define the RF inspection and its acceptance conditions
PIM is central to this article, but it is only one part of passive-component acceptance. Depending on the product type, a review may also include parameters such as VSWR or return loss, insertion loss, coupling value, isolation, attenuation, port balance, frequency range, and power rating.
RFCOM uses end-of-line RF inspection for applicable product families. The inspected parameters, sampling or inspection scope, test setup, and acceptance thresholds must be confirmed for the selected model and order.
For PIM in particular, the test record should be understandable without relying on a single number. The buyer should be able to identify the product model and connector configuration; test frequencies; applied test-tone power; method and duration; static or dynamic condition; acceptance threshold and result; and test date and record identifier where agreed.
Selected RFCOM passive-component models may be specified at -160 dBc PIM, subject to product type, connector configuration, frequency band, and test conditions. This is not a portfolio-wide guarantee. The approved datasheet and agreed test basis for the exact model remain the controlling documents.
5. Separate RF performance from environmental qualification
A PIM measurement and an environmental qualification answer different questions. A PIM test describes performance under a stated measurement condition. Environmental tests may evaluate how a product family responds to factors such as corrosion exposure, vibration, temperature, or transport stress.
Applicable RFCOM product families may undergo qualification testing selected for their intended use. The test type, duration, severity, sample basis, and pass criteria are model- or family-specific. We therefore do not apply a universal salt-spray duration, vibration test, ingress rating, or outdoor-use statement to the complete passive portfolio.
For an outdoor DAS or BTS application, the buyer should confirm the relevant environmental requirements alongside the RF specification. For an indoor project, the required qualification plan may be different. In both cases, the acceptance basis should be written into the approved specification or order documents.
6. Agree the delivery evidence before production
Quality is easier to verify when both parties know what evidence will accompany the product. The documentation package should be defined at the same time as the technical requirement.
Depending on the model, order, and agreed quality plan, the package may include an approved specification or drawing, inspection or test records, traceability information, labeling details, packing information, and agreed acceptance documents. Availability and format must be confirmed before quotation or order release.
| What to define | Why it matters | Evidence to review |
|---|---|---|
| Exact model and RF function | Prevents a family-level statement from being treated as a model guarantee | Approved datasheet or drawing |
| Band, power, and connector configuration | Establishes the operating and mechanical context | Approved technical specification |
| PIM target and test conditions | Makes the result comparable and auditable | Agreed test method and acceptance limit |
| Other RF parameters | Confirms the required network function | Applicable RF inspection results |
| Indoor or outdoor environment | Links qualification to the installation | Model-specific environmental evidence |
| Traceability and delivery records | Clarifies buyer acceptance evidence | Agreed quality and documentation plan |
This approach avoids approving a product on a marketing description and trying to reconstruct acceptance criteria only after shipment.
7. Treat the component as part of the complete RF path
Even a correctly specified low-PIM component cannot guarantee the PIM result of an installed DAS or BTS RF path. The final result can also be affected by cables and jumpers, connector condition, installation, contamination, corrosion, mechanical stress, nearby metalwork, power levels, and the test method used at the site.
That is why RFCOM keeps the component claim narrow. We can help select and review passive components for a defined application, but the site result must be assessed across the complete RF path. Field diagnosis and site-level PIM troubleshooting should follow a separate engineering process.
8. What to send RFCOM for a model review
- network topology or relevant RF-path diagram;
- required component type and port configuration;
- operating bands and frequency range;
- connector interface and gender;
- average and peak power requirements;
- required PIM level and test conditions;
- other applicable RF parameters;
- indoor or outdoor conditions and required environmental rating;
- quantity, delivery destination, and schedule requirement; and
- documentation, labeling, packing, traceability, or acceptance requirements.
If the project is still at an early stage, RFCOM can review the available information and identify which items must be confirmed before model selection or quotation.
Consistency comes from a defined chain
Consistent low-PIM delivery is not built around one impressive number. It comes from a clear requirement, a suitable product-family design, controlled assembly, a defined RF inspection plan, applicable qualification, and an agreed evidence package.
For buyers, the most useful question is not simply, “What is the PIM value?” It is, “Which model, under what conditions, and what evidence will support acceptance?”
RFCOM supplies passive components for DAS, indoor coverage, BTS and tower-site RF paths. To review a requirement, share your band plan, component list, connector configuration, power level, PIM target, environment, and acceptance needs through RFCOM Support.
